Understanding Coastdown in Rotating Machinery Analysis







Coastdown — also called rundown or deceleration — is the process of letting a rotating machine slow from operating speed to a stop with no active braking, relying on the natural losses of friction, windage, and bearing drag. In rotor dynamics and vibration analysis, a coastdown test is a diagnostic procedure in which vibration data is recorded continuously as the machine decelerates, yielding rich information about critical speeds, natural frequencies, and the system’s dynamic character. Together with its mirror-image, the runup test, it is a foundational tool for commissioning new equipment, troubleshooting stubborn vibration, and validating rotordynamic models against the machine as actually built and installed.
1. Purpose and Applications
Critical-Speed Identification
The headline use of coastdown testing is locating critical speeds:
- as speed falls through each critical speed, the vibration amplitude peaks;
- peaks in the amplitude-versus-speed plot mark the critical speeds;
- an accompanying 180° phase shift confirms it is true resonance rather than another speed-related effect; and
- several critical speeds can be captured in a single run.
Natural-Frequency Measurement
Critical speeds correspond to natural frequencies:
- the first critical speed occurs at the first natural frequency, the second critical at the second, and so on;
- the test gives experimental confirmation of analytical predictions; and
- it is widely used to validate finite-element models.
Damping Determination
The sharpness of each resonance peak reveals the system damping:
- sharp, high peaks indicate low damping;
- broad, low peaks indicate high damping;
- the damping ratio can be calculated from the peak’s width and amplitude; and
- that figure is critical for predicting vibration levels in future operation.
Unbalance-Distribution Assessment
- phase relationships at the critical speeds reveal how the unbalance is distributed along the rotor;
- they can distinguish static from couple unbalance; and
- they help plan the balancing strategy before any weight is added.
2. Coastdown Test Procedure
Preparation
- Install sensors: place accelerometers or velocity transducers at the bearing locations, in both horizontal and vertical directions.
- Install a tachometer: an optical or magnetic tachometer to track rotational speed and provide the phase reference.
- Configure data acquisition: set up continuous recording at an adequate sample rate.
- Define the speed range: typically from operating speed down to 10–20% of it, or until the machine stops.
Execution
- Stabilise at operating speed: run at normal speed until thermal equilibrium and steady vibration are reached.
- Initiate coastdown: disconnect drive power — motor, turbine, or other prime mover — and allow natural deceleration.
- Monitor continuously: record vibration amplitude, phase, and speed throughout the slowdown.
- Watch for safety: stay alert for excessive vibration that signals an unexpected resonance or instability.
- Complete deceleration: keep recording until the machine stops or reaches the minimum speed of interest.
Data-Collection Parameters
- Sample rate: high enough to capture every frequency of interest — typically 10–20× the maximum frequency.
- Duration: set by rotor inertia, anywhere from 30 seconds to 10 minutes.
- Measurements: amplitude, phase, and speed at all sensor locations.
- Synchronous sampling: data taken at constant angular increments to support order analysis.
3. Data Analysis and Visualisation
Bode Plot
The standard view of coastdown data is the Bode plot:
- upper trace: vibration amplitude versus speed;
- lower trace: phase angle versus speed;
- critical-speed signature: an amplitude peak with its matching 180° phase shift; and
- per location: separate plots for each measurement point and direction.
Waterfall Plot
A waterfall plot (cascade diagram) gives a three-dimensional view:
- X-axis: frequency (Hz or orders);
- Y-axis: speed (rpm);
- Z-axis (colour): vibration amplitude;
- the 1× component appears as a diagonal line tracking speed;
- natural frequencies appear as horizontal lines at constant frequency; and
- their intersection — where the 1× line crosses a natural-frequency line — is a critical speed.
Polar Plot
- vibration vectors are plotted at many speeds;
- a characteristic spiral forms as speed decreases through each critical speed; and
- the phase change is clearly visible as the vector sweeps round.
4. Coastdown vs. Runup Testing
Coastdown Advantages
- No external power required: simply disconnect the drive and let the machine coast.
- Slower deceleration: more dwell time at each speed gives better frequency resolution.
- Safer: the system is shedding energy rather than gaining it.
- Less stress: critical speeds are passed on falling energy.
Runup Advantages
- Controlled acceleration: the rate through critical speeds can be commanded.
- Part of normal startup: a run-up analysis can be gathered during a routine start.
- Active conditions: process loads are present, so the data is more representative of real operation.
Comparison Considerations
- Temperature: runup is usually performed cold; coastdown starts from hot operating conditions.
- Bearing stiffness: may differ between hot (coastdown) and cold (runup).
- Friction and damping: both are temperature-dependent and shift the peak amplitudes.
- Data comparison: differences between runup and coastdown traces can themselves reveal thermal or load effects.
5. Applications and Use Cases
New-Equipment Commissioning
- verify that critical speeds match the design predictions;
- confirm adequate separation margins;
- validate the rotordynamic model; and
- establish baseline data for future reference.
Troubleshooting Vibration Problems
- determine whether high vibration is speed-related (a resonance);
- uncover previously unknown critical speeds;
- assess the effect of a modification or repair; and
- separate resonance from other vibration sources.
Balancing Procedures
- for flexible rotors, coastdown identifies which modes need balancing;
- it helps choose the right balancing speeds; and
- it verifies the improvement after modal balancing.
Modification Verification
- after bearing changes, confirm the resulting critical-speed shift;
- after mass or stiffness changes, check the predicted natural-frequency change; and
- compare before-and-after coastdowns to quantify the improvement.
6. Best Practices for Coastdown Testing
Safety Considerations
- make sure everyone nearby knows the test is in progress;
- watch vibration closely for unexpected resonances;
- keep an emergency-shutdown capability available;
- clear the area around the equipment; and
- if excessive vibration develops, consider an emergency stop rather than finishing the coastdown.
Data Quality
- Right deceleration rate: not so fast that there are too few data points per speed, nor so slow that thermal conditions drift during the run.
- Stable conditions: minimise process-variable changes during the test.
- Multiple runs: perform two or three coastdowns to verify repeatability.
- All locations at once: record every bearing simultaneously.
Documentation
- record the operating conditions — temperature, load, configuration;
- capture the complete vibration and speed data;
- generate the standard analysis plots (Bode, waterfall, polar);
- identify and mark every critical speed found; and
- compare against design predictions or previous test data, then archive it.
7. Interpretation of Results
Identifying Critical Speeds
- look for amplitude peaks in the Bode plot;
- confirm each with its 180° phase shift;
- note the speed at which the peak occurs; and
- calculate the separation margin from operating speed.
Assessing Severity
- Peak amplitude: how high does vibration climb at the critical speed?
- Peak sharpness: a sharp peak means low damping and a potential problem.
- Operating proximity: how close is the running speed to a critical speed?
- Acceptability: a separation margin of about ±15–20% is typically required.
Advanced Analysis
- extract mode shapes from multi-point measurements;
- calculate damping ratios from the peak characteristics;
- distinguish forward from backward whirl modes; and
- compare the results against Campbell diagram predictions.
8. Coastdown in the Field
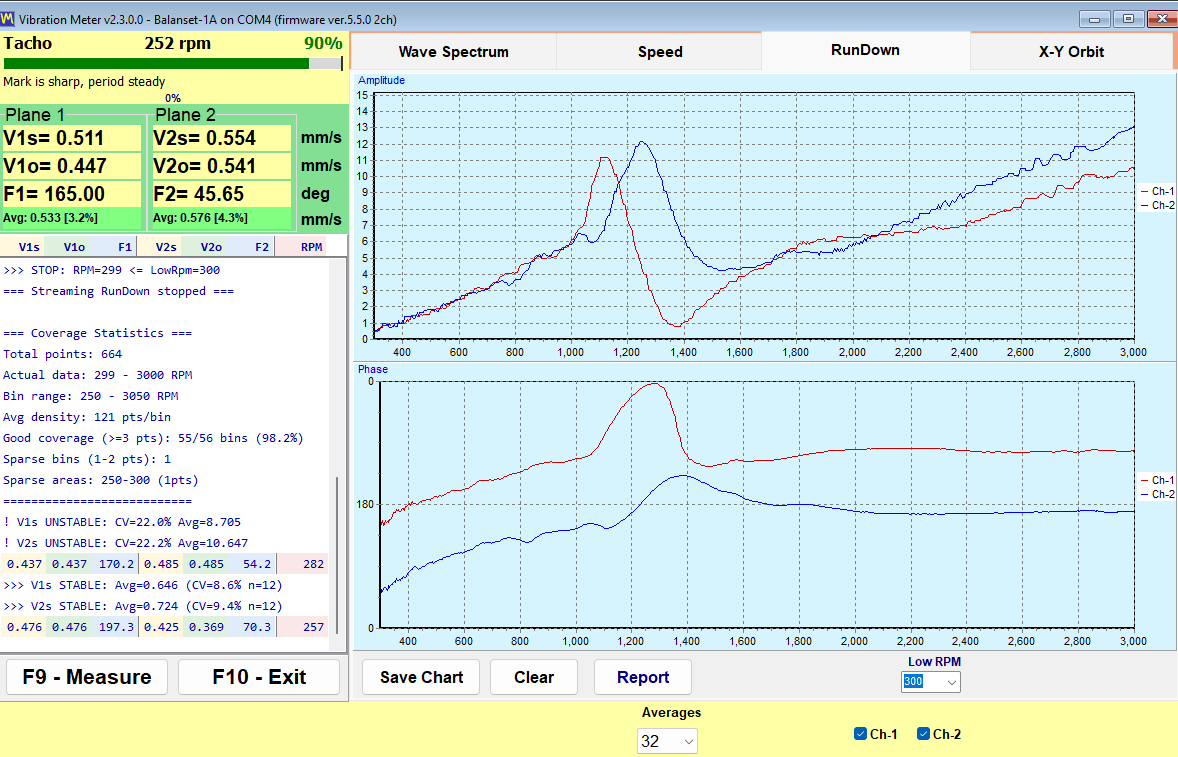
On site, a coastdown does not require a dedicated test stand — it can be captured with a portable instrument the moment the drive is switched off. A two-channel analyser such as the Balanset-1A, with its laser tachometer providing the phase reference, records amplitude, phase, and speed continuously as the rotor slows, so the engineer can read the critical-speed peaks straight off the resulting Bode trace. The same dataset that locates a resonance also confirms whether a 1× unbalance is contributing, letting diagnosis and a follow-up field balancing job flow from a single run-down. In short, coastdown testing supplies empirical data that complements analytical prediction and reveals the genuine dynamic behaviour of rotating machinery under real operating conditions.
What the Instrument Does During the Coast
The sequence on a Balanset-1A mirrors the procedure above. Bring the machine to operating speed and press F9 on the “Run-down” tab: the program first captures a reference measurement at working speed (“Capturing baseline…”), then prompts that the rotor can be stopped. From that moment it records the 1× amplitude and phase on every revolution while the speed readout tracks the falling RPM, and recording ends by itself once speed drops below the “Low RPM” threshold (100–2000 RPM, default 300).
The points are plotted as measured — one per revolution, no averaging. On machines where the synchronous component genuinely alternates from turn to turn (looseness, rubbing, a 2:1 belt drive) the visible comb of alternating points is real signal, not display noise; where the tachometer mark is lost, the chart shows gaps instead of inventing straight lines.
The full report bundles the amplitude and phase curves with the snapshots taken at working speed — waveform, spectrum, tacho-mark intervals and the X-Y orbit — so the coast and the pre-coast state of the machine travel in one document.